
Why Choose Top Chain Conveyor for Global Buyers?
Global buyers are rethinking conveyor investment as labor costs, product variety, and delivery expectations continue to rise. Grand View Research estimates that the global conveyor systems market reached approximately USD 7.6 billion in 2023. Its forecast also indicates steady growth through 2030. Meanwhile, the MHI 2024 Annual Industry Report found that 55% of supply chain leaders planned to increase technology and innovation investment. These figures reveal a practical concern: factories need reliable movement, not merely faster equipment.
A Top Chain Conveyor can support that objective through stable product handling, modular construction, and precise transfer between processing stages. Its chains can carry cartons, trays, bottles, or heavier packaged goods across humid, dusty, or washdown areas. Dr. Michael ten Hompel, a respected German intralogistics researcher, has described logistics as the controlled movement of goods, information, and people. That principle matters here. A conveyor must fit the complete flow.
No conveyor is universally best. That assumption deserves testing. Buyers should compare load weight, chain material, sanitation requirements, noise levels, maintenance access, and local service capacity. A low purchase price may become expensive when sprockets, bearings, or spare chains are unavailable. In my experience, the strongest projects begin with a site walk, not a catalog. Operators often notice details that specifications miss, such as awkward handoffs or difficult cleaning points. For global buyers, choosing a Top Chain Conveyor is therefore less about selecting a machine and more about securing dependable performance across real operating conditions.
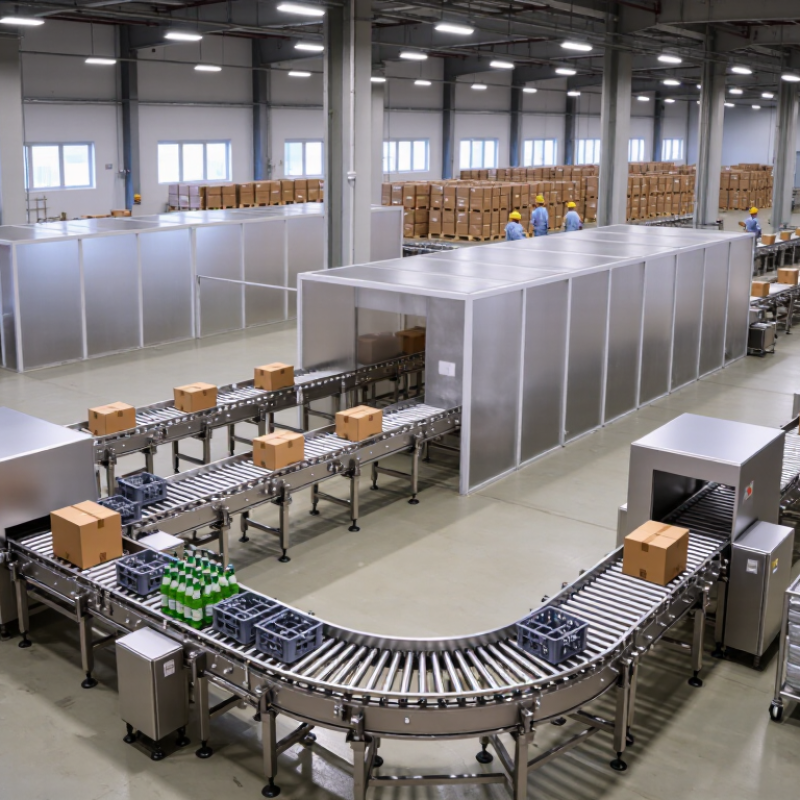
Top Chain Conveyor Basics: Modular Belts and 5–60 m/min Typical Speeds
Why Choose Top Chain Conveyor for Global Buyers?
Top chain conveyors use linked modular belts to move bottles, cartons, trays, and packaged goods with controlled contact. Each belt section can be replaced individually, which simplifies routine maintenance and reduces unnecessary downtime. Common belt materials include stainless steel and engineered plastics, selected according to temperature, moisture, friction, and sanitation requirements. Sprockets guide the belt, while wear strips support smooth movement along the conveyor frame.
Typical operating speeds range from 5 to 60 m/min. Lower speeds suit fragile containers, accumulation zones, or products requiring careful positioning. Higher speeds can support steady packaging lines when the load is stable and the layout is properly calculated. Speed alone does not define performance. Product spacing, belt width, conveyor length, incline angle, and motor torque also matter. A lightweight carton may travel well at 45 m/min, while unstable bottles may need a slower setting. That matters.
Experienced integrators usually confirm these conditions before selecting components. They check belt tension, transfer gaps, cleaning access, and the available floor space. Global buyers should also request clear documentation for materials, electrical specifications, guarding, and maintenance intervals. Local voltage and safety expectations may differ. Small design errors can become expensive later. In practice, the 5–60 m/min range is useful, but it is not universal. Real production tests may reveal vibration, noise, or product movement that calculations miss. That is where careful adjustment begins.
| Selection Dimension | Typical Data or Range | Technical Meaning | Global Buyer Relevance |
|---|---|---|---|
| Conveyor Type | Plastic modular belt with sprocket drive | Interlocking belt modules form a continuous conveying surface. Sprockets engage the belt positively, reducing slip compared with friction-driven flat belts. | Flexible layout |
| Typical Operating Speed | 5–60 m/min | The practical speed depends on product stability, belt material, conveyor length, incline, loading pattern, and the required throughput. | Application dependent |
| Belt Surface Styles | Flat-top, flush-grid, perforated, ribbed, and roller-top | Flat-top surfaces support stable transport; flush-grid surfaces improve drainage and airflow; ribbed or roller-top surfaces can assist with incline or accumulation applications. | Product matching |
| Common Belt Materials | Polypropylene (PP), polyethylene (PE), and acetal (POM) | PP is commonly selected for general conveying and higher-temperature conditions than PE. PE offers good impact and chemical resistance. POM provides low friction and dimensional stability. | Material choice |
| Operating Temperature | Approximately −40 to 90 °C, depending on polymer grade | The usable range varies by belt resin, load, speed, cleaning method, and exposure time. The belt supplier’s technical datasheet should be checked before specification. | Environment check |
| Belt Width | Commonly 100–1,500 mm; custom widths may be available | Width should be selected according to product dimensions, side clearance, loading pattern, belt pull, and available installation space. | Capacity planning |
| Modular Belt Pitch | Typical pitches include 12.7, 25.4, 38.1, and 50.8 mm | Pitch is the distance between corresponding points on adjacent modules. Smaller pitches generally provide a smoother transfer, while larger pitches may suit heavier-duty conveying. | Transfer quality |
| Conveyor Configuration | Straight, incline, decline, curve, or Z-frame | Modular belt systems can be configured for different routes. Curves and inclines require suitable belt design, sprockets, guides, and product-control features. | Space efficiency |
| Incline Capability | Often about 5–20° for standard conveying | The practical angle depends on surface pattern, product packaging, coefficient of friction, speed, acceleration, and the need for flights or side guards. | Layout dependent |
| Drive Arrangement | Head drive or center drive with geared motor | Drive selection is based on belt pull, conveyor length, speed, product load, incline, starts per hour, and operating duty. | Power sizing |
| Typical Applications | Food processing, beverage packaging, logistics, personal care, and general manufacturing | The open or solid belt surface can be selected for drainage, sanitation, product stability, accumulation, or general unit-load transport. | Industry fit |
| Cleaning and Maintenance | Tool-assisted belt removal; washdown depends on frame and component design | Modular belts can be repaired by replacing individual modules or hinge rods. Hygienic designs require suitable clearances, materials, drainage, and compatible cleaning chemicals. | Lower downtime |
| Product Transfer | Transfer quality depends on pitch, nose-bar design, pulley diameter, and product size | Small products and short gaps typically require a suitable small-pitch belt or transfer arrangement to reduce tipping and product loss. | Product protection |
| Load Capacity | Project-specific; determined by belt pull and frame design | There is no universal load rating. Calculation should consider distributed load, belt width, conveyor length, friction, incline, speed, start-up torque, and support spacing. | Engineering review |
| International Specification Items | Voltage, frequency, guarding, electrical protection, documentation, and applicable local standards | Global projects should confirm motor voltage and frequency, emergency-stop requirements, guarding, spare parts, installation instructions, and language requirements before order approval. | Project readiness |
Note: The figures shown are typical engineering ranges for preliminary selection only. Final performance depends on the complete conveyor design, belt specification, conveyed product, operating environment, and applicable safety requirements.